Sourcing pneumatic tool component die casting begins with matching part size to machine tonnage and confirming which secondary operations run in house. A quotation should carry tooling cost, piece prices at several volumes and DFM feedback. Mold ownership belongs in the contract. Tooling runs roughly 65 to 90 days to first approved parts.
JoinCast has supplied pneumatic tool die casting from Changhua, Taiwan since 1987. This article sets out what we would check when evaluating a casting supplier: capacity, in-house scope, tooling terms and the parts of landed cost that never appear on the piece price line. Figures here are ours and are current as of August 2026.
What to check in a pneumatic tool component die casting supplier
A supplier’s machine range, in-house scope, quality certification and inspection equipment can all be checked before you send a drawing anywhere. Ask for all four, and you will know whether the plant can build the part as well as price it.
Machine tonnage against part size and weight
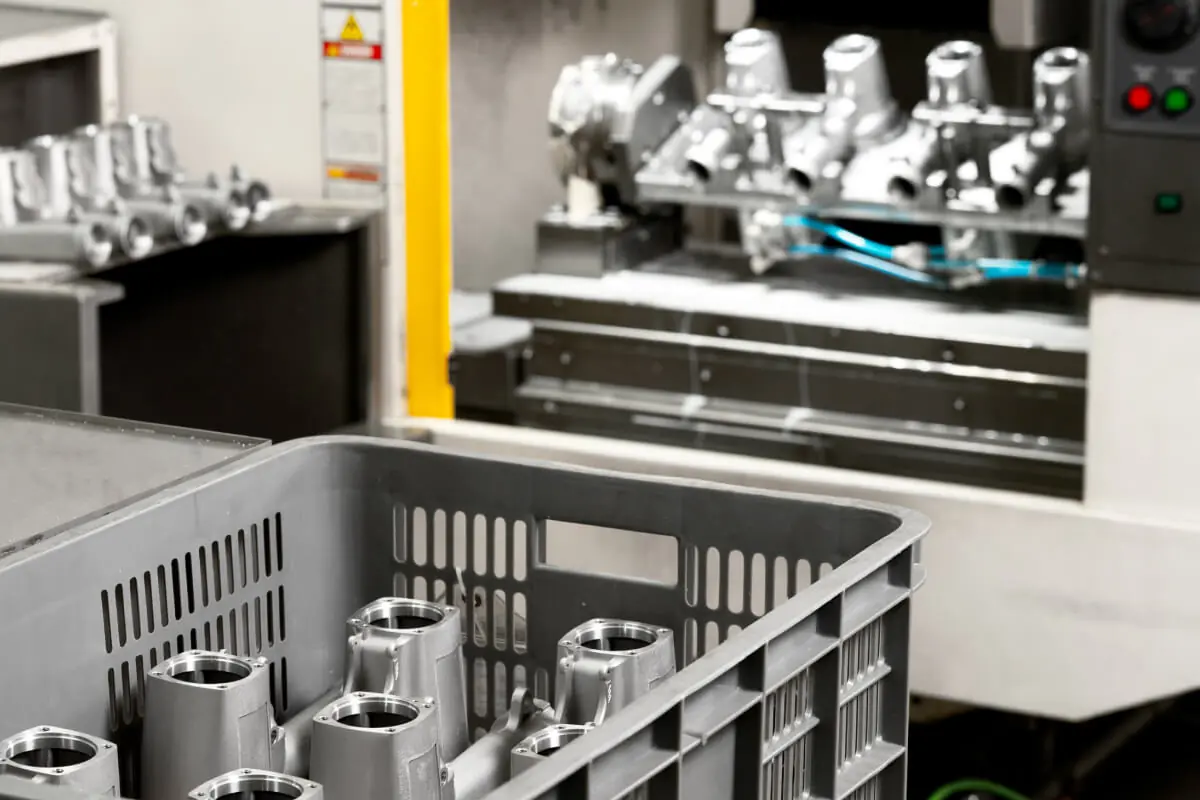
Our twelve die casting machines run from 135 to 900 tons, covering parts up to 700 mm and weights of 5 grams to 3 kilograms. If a supplier’s largest machine barely accommodates your part, there’s no room for a second cavity or a heavier variant later. Ask for the tonnage list with the part size each machine takes, then hold your current part and its likely successor against it.
Volume is the second constraint. Our minimum order quantity is 2,000 pieces for a simple single-cavity part and complex multi-cavity molds, 1,000 pieces for large castings from the 900 ton machine, which reflects the tooling investment behind each. If a supplier’s minimum sits well above your annual call-off, you will be buying stock you then have to hold, and that cost belongs in the comparison.
In-house scope, certification and inspection equipment
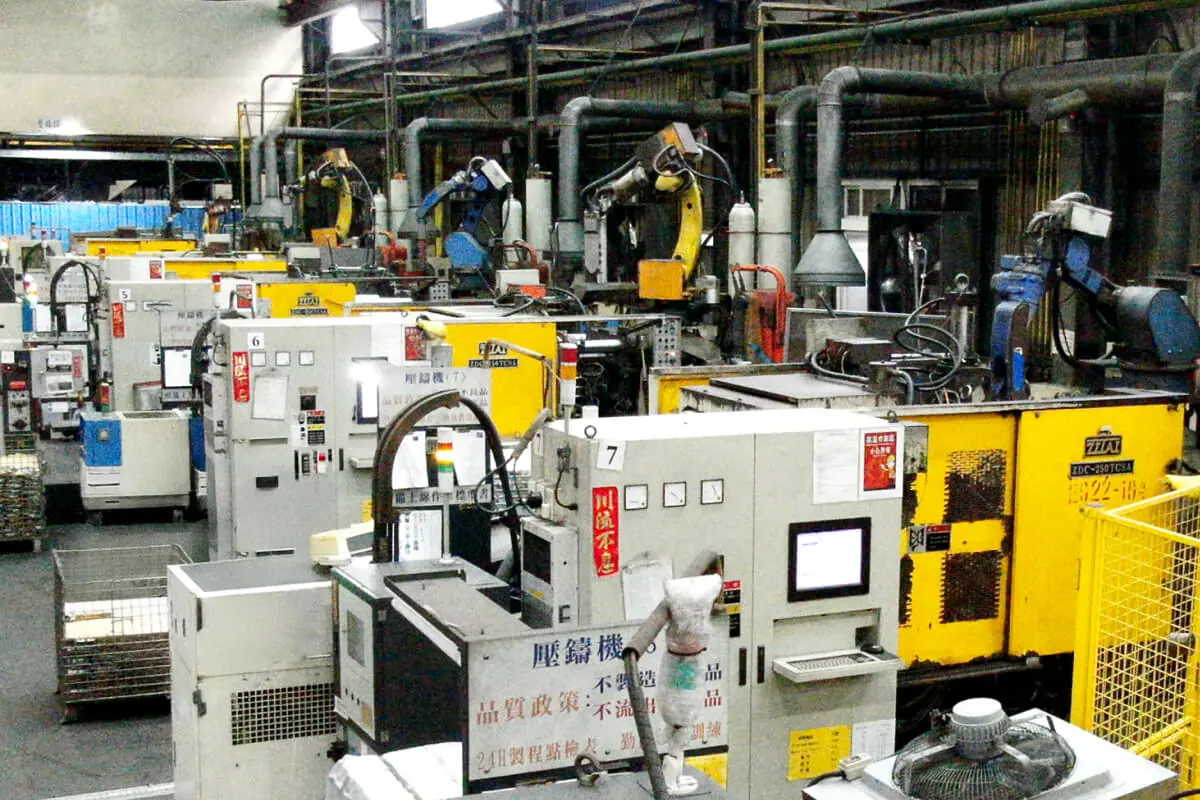
Casting is rarely the whole scope on a tool component. Machining, polishing, shot blasting, coating and grip overmolding all follow. Each transfer between companies adds handling and transport, and if a part is rejected later, gives the two firms something to argue about. We perform all of these in one 9,900 square meter plant, with 49 CNC machining systems, eight polishing machines, three shot blasting systems and automated surface treatment lines. Ask which operations a supplier subcontracts, and to whom.
JoinCast holds ISO 9001:2015 certification, and as of August 2026 the 2015 edition remains current with a new edition in preparation at ISO, so a certificate you review this year may carry a transition date. Certification confirms that a quality system exists and is audited each year. It does not tell you whether the plant can hold your tolerances. For that, look at the inspection equipment and at the first article data. Our ten-person quality team runs two Mitutoyo CMMs, a Keyence 3D scanner, an aluminum spectrometer returning an elemental analysis in about 60 seconds, surface roughness testers and a salt spray tester, and we keep statistical process control documentation on high-volume orders. Ask any shortlisted supplier for a sample first article report. It will show you what they measure and how they record it.
What single source manufacturing changes about the quotation
A single supplier performing casting, machining and finishing quotes one price for a finished component, so you can’t compare that figure against a casting-only price without adding the operations that follow it.
Handoffs, responsibility and cost
Every transfer between companies carries cost that rarely appears as a line on a quotation: packing for transit, inbound inspection at the next supplier, and the working capital tied up while parts move between sites. Where casting and machining sit in one building, the team that cast the part also measures it, so we catch a drifting dimension on site and correct it there.
Settle responsibility before you place tooling. With one supplier for the finished component, the casting, the machining and the coating are all our responsibility, and there’s no argument about which company caused a rejected part. With three suppliers the commercial position depends on your contracts, and resolving it takes time.
How to read a delivery performance figure
We state a 99% reliable delivery rate. Whatever figure a supplier quotes, ask how it is measured, over what period, and whether partial shipments count as on time. In practice the definition tells you more than the number.
What the tooling stage commits you to
Once you have paid for tooling, changing supplier becomes expensive, so the terms deserve rather more attention than the piece price.
Lead time, quotation content and sampling
We design, build and sample a new tool in around 65 to 90 days before the first approved parts, and we provide a production schedule after contract signing rather than at quotation, since the schedule depends on the size, tonnage and complexity of the mold. Our engineering team returns quotations within 5 to 7 business days, including DFM feedback, process recommendations, tooling cost, piece prices at various volumes and estimated timelines. We complete first article inspection before full production begins, comparing scan data against your CAD model. A quotation that arrives without DFM comment suggests the drawing wasn’t read closely.
Mold ownership and storage
Mold ownership at JoinCast is negotiable and specified in your contract. Whoever owns it, the mold stays in our Changhua facility for the life of the project, so maintenance and later modification stay with the team that built it. Record ownership, transfer conditions and maintenance responsibility in writing before tooling starts. That’s advice, and it applies to any supplier you use, not only to us.
How to compare pneumatic tool component die casting quotations
Piece price is only one of the costs you carry over the life of the project. Tooling amortization, duty treatment, freight, inspection at goods-in and the cost of a quality escape all sit alongside it, and engineering time is the easiest of them to overlook. A supplier who reviews your CAD data at quotation and returns alloy and tolerance feedback on tool housings does work your own team would otherwise have to repeat once the first samples arrive.
Duty and tariff treatment as of August 2026
USTR announced Section 301 tariffs on 23 July 2026 covering 60 economies, with Taiwan in a band of 10 to 12.5 percent net of MFN rates. The USTR fact sheet excludes “all articles and parts of articles subject to section 232 tariffs” from that action, so classification determines what you actually pay. The position changes, and any figure in a cost model should carry the date it was taken. Our comparison of tariff and IP differences between Taiwan and China covers this in more detail, alongside the wider case for sourcing aluminum die casting from Taiwan.
What to request in the RFQ
| What to request | Why it matters | A weak answer |
|---|---|---|
| Machine tonnage list with part size per machine | Confirms your part and its successors fit the plant | A single tonnage figure with no range |
| Which operations are subcontracted | Locates the handoffs and the responsibility boundaries | “Everything is handled” with no list |
| Sample first article inspection report | Shows what the supplier measures and how it is recorded | A certificate with no dimensional data |
| Tooling cost, ownership and storage terms | Determines what you own and what changing supplier would cost | Ownership left to the invoice |
| Piece price at several annual volumes | Makes tooling amortization visible | One price at one volume |
| Minimum order quantity by part type | Sets your call-off and inventory position | A single MOQ for all parts |
| Quotation turnaround and DFM feedback | Indicates how closely the drawing was read | A price with no engineering comment |
Frequently asked questions about pneumatic tool component die casting
What is the minimum order quantity for a die cast tool component?
JoinCast sets a minimum of 2,000 pieces for simple single-cavity parts and complex multi-cavity molds, 1,000 pieces for large castings from the 900 ton machine. The difference reflects the tooling investment each requires. Annual volume also affects piece price, so we quote at several volumes.
How quickly can you quote, and what does the quotation include?
JoinCast engineering returns quotations within 5 to 7 business days. Each one includes DFM feedback on the part, process recommendations, tooling cost, piece prices at various volumes and estimated timelines. We provide a production schedule after contract signing, since it depends on mold size, tonnage and complexity.
Who owns the mold?
Mold ownership at JoinCast is negotiable and recorded in the contract. Whoever owns it, the mold remains in our Changhua facility for the life of the project, which keeps maintenance and modification with the team that built it. Settle ownership and transfer conditions in writing before tooling begins.
What certification does JoinCast hold?
JoinCast is certified to ISO 9001:2015, covering quality management across production. As of August 2026 that edition remains current, with a new edition in preparation at ISO. We also hold first article inspection data and statistical process control records, and those, rather than the certificate, show whether we can hold your tolerances.
What part sizes and volumes suit your plant?
JoinCast runs twelve die casting machines from 135 to 900 tons, covering parts up to 700 mm and weights of 5 grams to 3 kilograms, supported by 49 CNC machining systems and in-house surface treatment. Parts outside that range are better placed elsewhere, and we will tell you so at enquiry rather than after tooling.
How do current tariffs affect castings sourced from Taiwan?
USTR announced Section 301 tariffs on 23 July 2026 covering 60 economies, with Taiwan in a 10 to 12.5 percent band net of MFN rates, and the accompanying fact sheet excludes articles subject to section 232 tariffs. Classification determines what applies to a given part. Figures are current as of August 2026, so check them against the USTR notice before you put them into a cost model.